In today’s fast-paced manufacturing and logistics environments, efficient material handling is essential for productivity and cost control. An automation chain conveyor solution provides a reliable and scalable way to transport heavy loads, streamline workflows, and improve overall operational efficiency.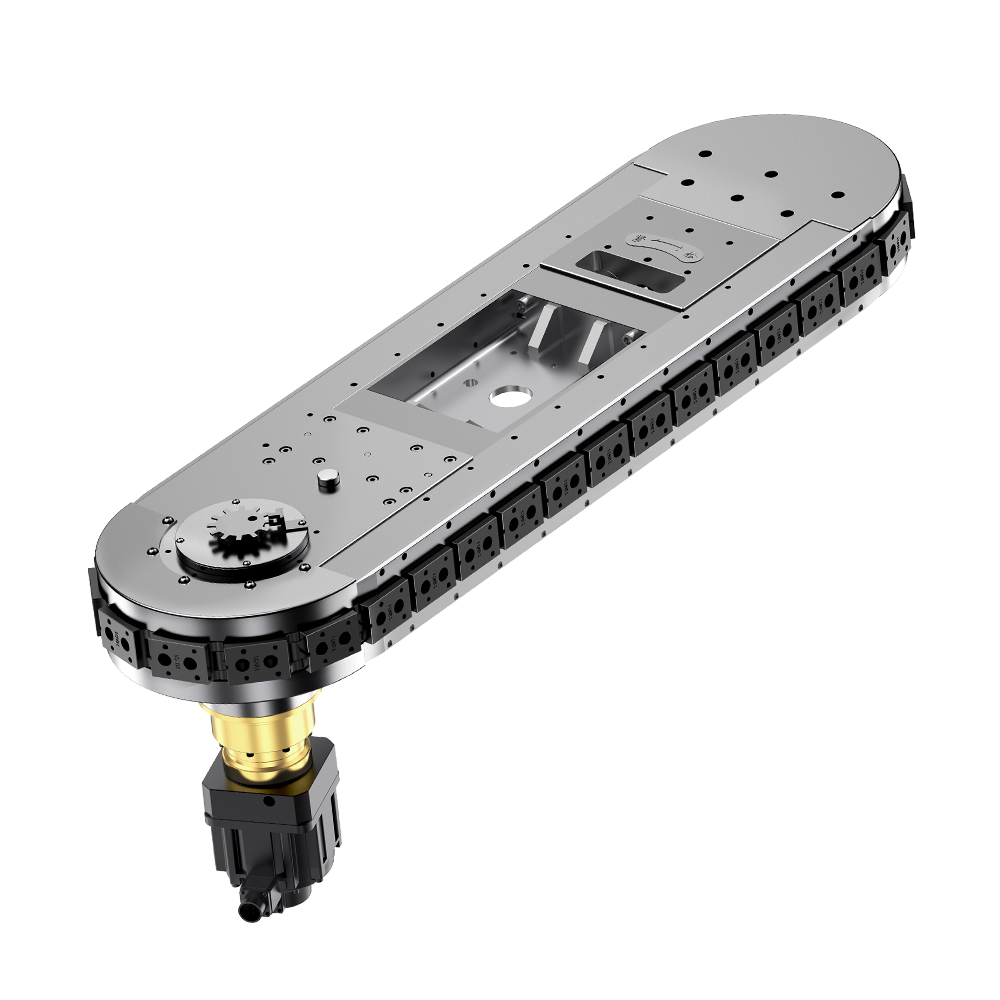
Chain conveyor systems are widely used in industries that require durable, high-capacity transport solutions. With the ability to handle complex layouts and heavy-duty applications, they are a key component in modern automated production lines.
An automation chain conveyor solution is a material handling system that uses chains to move products or pallets along a predefined path. These systems are designed for continuous operation and can be fully integrated into automated production or logistics systems.
Key components typically include:
Conveyor chains
Drive motors and gearboxes
Sprockets and guiding structures
Control systems and sensors
Supporting frames and structures
These components work together to ensure smooth, stable, and efficient product movement.
Chain conveyors are ideal for transporting heavy or bulky items such as pallets, metal parts, and industrial equipment. Their robust design ensures reliable performance under demanding conditions.
Compared to other conveyor types, chain conveyors offer excellent durability. They are built to withstand harsh environments, including high temperatures, dust, and heavy wear.
An automation chain conveyor solution can be customized to fit different layouts, including straight lines, curves, and multi-level systems. This flexibility allows seamless integration into existing production lines.
With proper design and lubrication, chain conveyors require minimal maintenance and offer long service life, reducing downtime and operational costs.
Chain conveyor systems are widely used across various industries:
Manufacturing and assembly lines
Automotive production
Warehouse and logistics systems
Packaging and distribution centers
Food and beverage processing
Heavy machinery and metal processing
In these applications, automation improves efficiency, reduces manual labor, and ensures consistent material flow.
Standard conveyor systems may not meet all operational requirements. That’s why many businesses choose custom automation chain conveyor solutions tailored to their specific needs.
Customization options include:
Conveyor length and layout design
Chain type and material selection
Load capacity optimization
Speed and control system configuration
Integration with robotics and automation equipment
A customized solution ensures optimal performance and better alignment with production goals.
When selecting an automation chain conveyor solution, consider the following factors:
Load type and weight: Determines chain strength and system design.
Conveyor speed: Impacts productivity and system efficiency.
Layout requirements: Straight, curved, or multi-level configurations.
Operating environment: Temperature, humidity, and exposure to contaminants.
Automation level: Integration with sensors, PLCs, and control systems.
Evaluating these factors helps ensure the system meets both current and future operational needs.
A reliable chain conveyor manufacturer is critical to the success of your automation project. Look for a supplier that offers:
Engineering design expertise
Custom manufacturing capabilities
High-quality materials and components
Strict quality control processes
Technical support and after-sales service
Partnering with an experienced manufacturer ensures a durable, efficient, and scalable conveyor solution.
As industries continue to automate and scale operations, the demand for efficient material handling systems is growing rapidly. An automation chain conveyor solution provides the strength, reliability, and flexibility needed to support modern production and logistics environments.
Whether used in manufacturing, warehousing, or heavy-duty applications, chain conveyor systems play a vital role in improving efficiency, reducing costs, and enhancing overall operational performance.
For businesses looking to optimize their material handling processes, investing in a customized chain conveyor solution is a smart and future-ready choice.