Discover our high-performance chain oval conveyor system designed for seamless material handling. Boost productivity, ensure stability, and adapt to diverse industrial needs with our premium oval chain conveyors.
In the fast-paced world of modern manufacturing and logistics, efficient material handling is the backbone of operational success. Businesses across industries are constantly seeking conveyor solutions that can streamline workflows, reduce downtime, and adapt to dynamic production demands. Enter the
chain oval conveyor system—a game-changing solution engineered to redefine how you move materials within your facility.
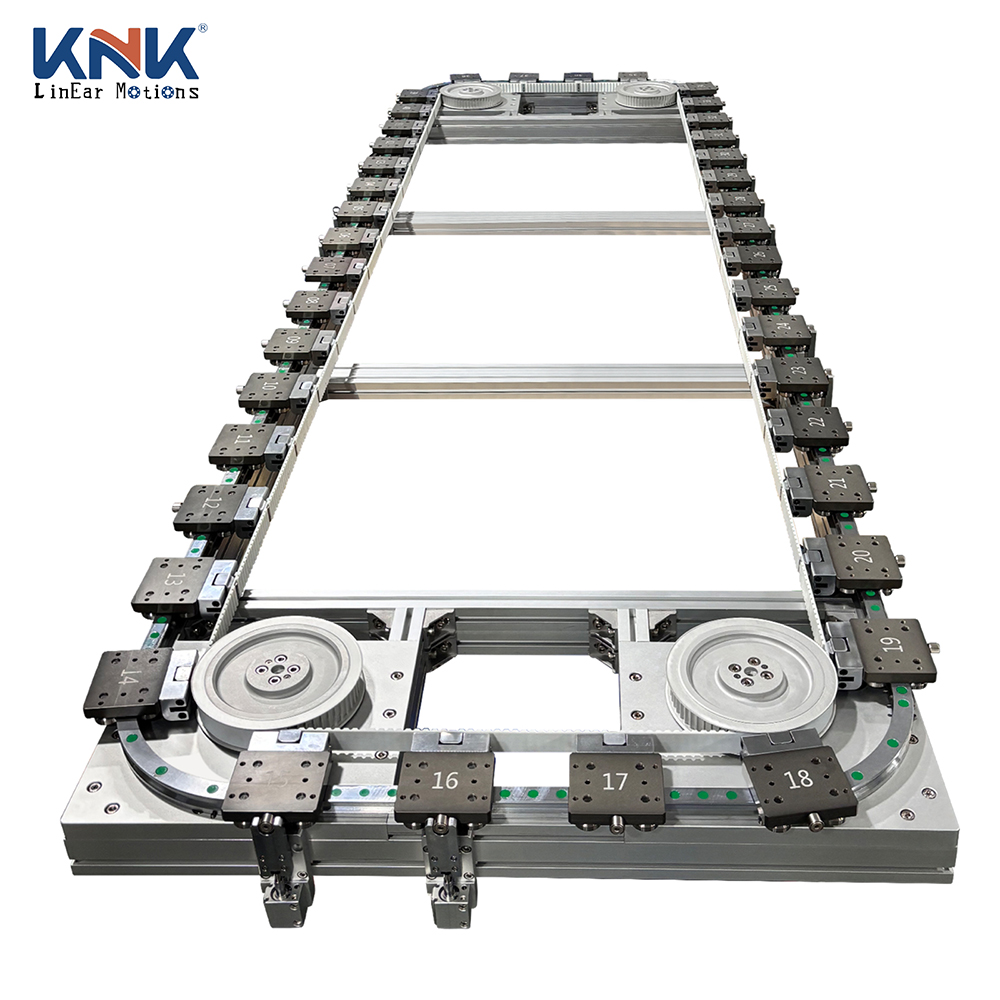
At KNK, we specialize in designing and manufacturing top-tier chain oval conveyor systems that cater to the unique needs of diverse industrial sectors. Our oval chain conveyors stand out for their robust construction, smooth operation, and exceptional versatility, making them the ideal choice for applications ranging from automotive assembly lines to food processing plants.
Why Choose a Chain Oval Conveyor System?
Unlike traditional linear conveyors, the chain oval conveyor system features a closed-loop, oval-shaped design that enables continuous material flow without the need for complex directional changes. This innovative structure offers numerous advantages that directly impact your bottom line:
1. Unmatched Operational Efficiency
The closed-loop design of our oval chain conveyor eliminates bottlenecks associated with loading and unloading zones. Materials move seamlessly around the oval track, ensuring a constant flow that maximizes throughput. Whether you’re transporting small components, heavy parts, or bulk materials, our conveyor system maintains consistent speed and performance, reducing production cycle times and boosting overall productivity.
2. Exceptional Durability & Reliability
Crafted from high-grade steel and precision-engineered components, our chain oval conveyor system is built to withstand the rigors of industrial environments. The heavy-duty chain mechanism resists wear, corrosion, and impact, ensuring long-term reliability with minimal maintenance. This durability translates to lower downtime, fewer replacement costs, and peace of mind knowing your conveyor will perform consistently even under heavy loads.
3. Flexible & Adaptable Design
We understand that every facility has unique layout and operational requirements. Ourchain oval conveyor systems are fully customizable, allowing for adjustments in track length, width, height, and speed to fit your specific space and application. Whether you need to integrate the conveyor with existing machinery, add auxiliary components like lifts or sortation devices, or adapt to changing production needs, our solution offers the flexibility to grow with your business.
4. Enhanced Safety & Ergonomics
Safety is a top priority in any industrial setting. Ouroval chain conveyor is equipped with advanced safety features, including guarded chain mechanisms, emergency stop controls, and anti-jam sensors, to minimize the risk of accidents. Additionally, the ergonomic design reduces the need for manual material handling, lowering the risk of worker fatigue and injury while improving overall workplace efficiency.
Versatile Applications Across Industries
The chain oval conveyor system’s adaptability makes it suitable for a wide range of industries, including:
-
Automotive: Transporting engine parts, body panels, and assembled components through production lines.
-
Food & Beverage: Handling packaged goods, raw ingredients, and containers with food-grade materials to meet hygiene standards.
-
Electronics: Moving delicate electronic components and devices with precision and care.
-
Logistics & Warehousing: Sorting, transporting, and accumulating packages for efficient order fulfillment.
-
Pharmaceuticals: Ensuring sterile and controlled transport of pharmaceutical products and medical devices.
Our Commitment to Excellence
At KNK, we don’t just sell chain oval conveyor systems—we deliver comprehensive material handling solutions tailored to your success. Our team of experienced engineers works closely with you to assess your needs, design a custom conveyor system, and provide seamless installation and ongoing support. We prioritize quality in every step of the process, from material selection to manufacturing and testing, ensuring that our conveyors meet the highest industry standards.
Investing in a chain oval conveyor system from [Your Company Name] is an investment in efficiency, reliability, and long-term operational success. Whether you’re looking to upgrade your existing conveyor system or implement a new material handling solution, we have the expertise and products to help you achieve your goals.
Ready to transform your production workflow with our premium chain oval conveyor system? Contact us today to request a free consultation and quote. Let our experts help you design the perfect conveyor solution for your business!